How Textile Brands Can Use Digital Printing for Limited Edition Collections
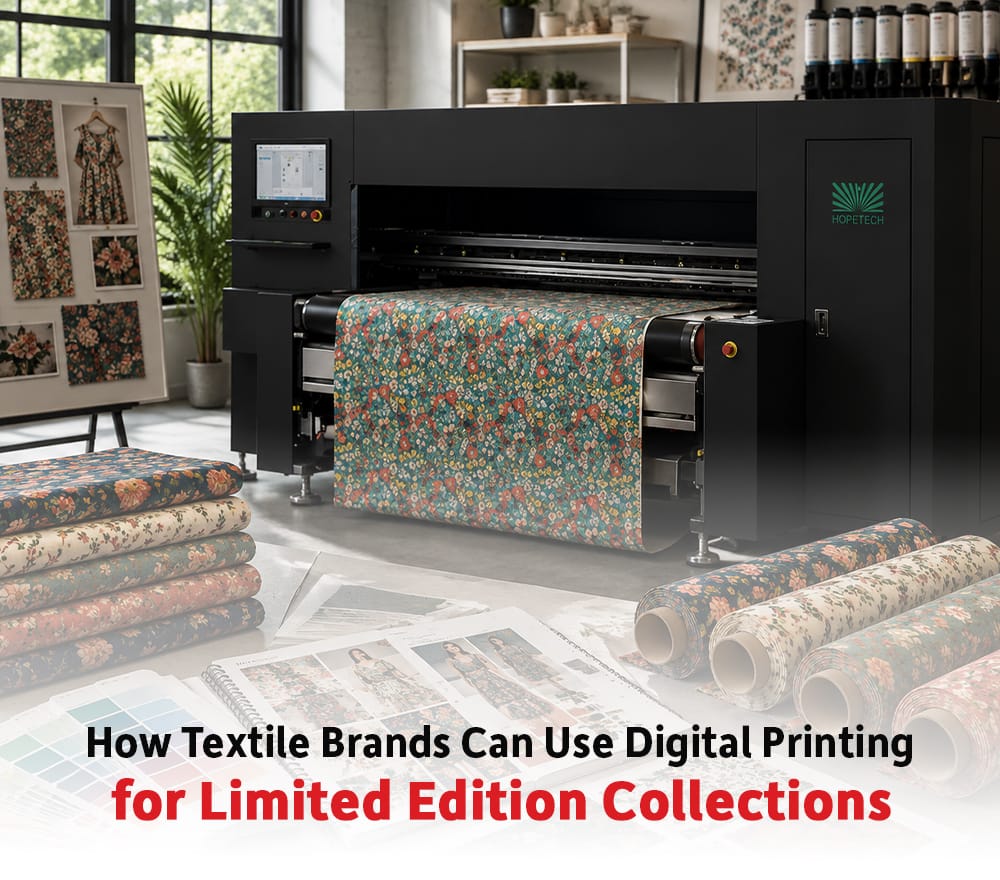
Limited Edition Collections Need Flexible Production Textile and fashion brands are increasingly using limited edition collections to create exclusivity and market excitement. These collections may be seasonal, festive, influencer-led, region-specific, or trend-based. Traditional production methods may not always be practical for such collections because quantities are smaller and design changes are frequent. Digital printing for limited edition textiles gives brands the flexibility to launch unique designs without committing to very large production volumes. This makes it easier to test ideas, create urgency, and respond to changing customer preferences. Small Runs Can Create Bigger Brand Value Limited edition collections often work because they feel special. Customers may respond better when a design is available only for a short time or in limited quantity. This approach can help brands build stronger engagement and reduce dependence on mass production. Digital textile printing supports this model because it allows smaller runs with high design variety. Brands can create capsule collections, festive prints, designer collaborations, custom drops, and exclusive fabric ranges with more control over production quantity. Faster Design Testing Reduces Risk Every new design carries risk. A print may look strong in concept but may not perform well in the market. With digital printing, brands can test limited quantities before committing to larger production. If a design performs well, it can be repeated. If it does not, the brand avoids large unsold inventory. This is especially useful for fashion labels, home textile brands, online sellers, and boutique businesses that need to stay fresh without overproducing. Customization Makes Collections More Attractive Limited edition textiles can become more powerful when combined with customization. Brands can create personalized prints, regional designs, special themes, or exclusive patterns for specific customer groups. Digital printing makes such customization easier because the artwork can be changed digitally without long setup processes. This helps brands create more meaningful product stories and stronger customer connection. Quality Still Defines the Collection A limited edition collection may be small in quantity, but it still needs high-quality production. Print sharpness, color consistency, fabric feel, finishing, and durability all affect how customers experience the product. Brands should work with production partners who understand both creativity and technical execution. The success of a limited edition textile collection depends on how well the design idea is converted into finished fabric. Conclusion Digital printing for limited edition textiles helps brands create exclusive collections, test new ideas, reduce inventory risk, and build stronger customer engagement. It gives textile brands the freedom to launch more creative products without being restricted by large production commitments. True Colors can support such collections by offering more than production capacity. Its ecosystem of digital printing machines, fabrics, Inkia by True Colors inks, True Colors Sublimation Paper, and technical expertise can help brands convert creative concepts into production-ready textile outputs. For limited edition collections, where every design needs to feel intentional and well-executed, True Colors brings the balance of flexibility, quality understanding, and production support that modern textile brands need.
Color Management in Textile Printing: From Design Screen to Final Fabric
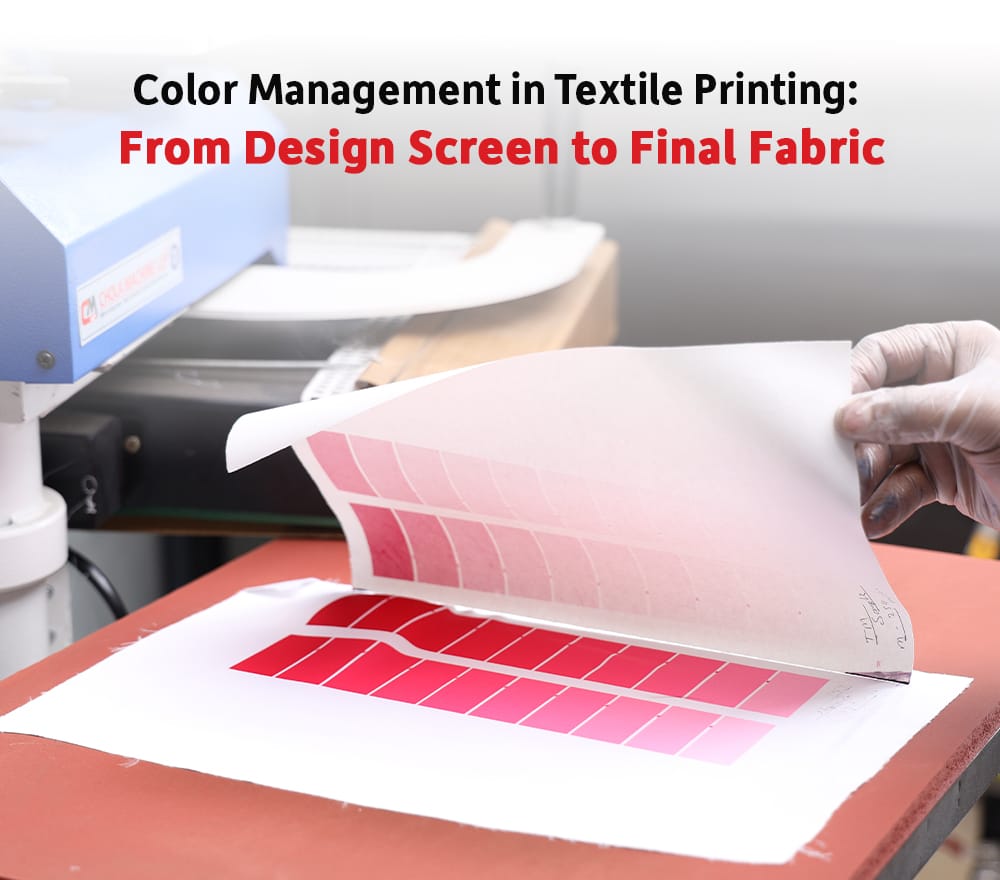
Color Changes Across the Printing Journey In textile printing, a design begins on a screen but ends on fabric. Between these two stages, many factors influence how the final color appears. Color management in textile printing helps reduce the gap between digital artwork and printed fabric. Without proper color control, manufacturers may face shade variation, repeated sampling, customer dissatisfaction, and production delays. This is why color management should be treated as an important part of the digital textile printing workflow. Screen Color Is Not Final Fabric Color Designers often approve artwork on monitors, but screen color is created through light while fabric color is created through ink, material absorption, printing process, and finishing. This means the same design can appear different on screen, paper, and fabric. Manufacturers should educate customers and internal teams about this difference. The goal of color management is not to make every screen look exactly like fabric, but to create a controlled and repeatable process that reduces unexpected variation. Fabric Type Influences Color Output Different fabrics produce different color results. Polyester, cotton, viscose, silk, blends, and other materials absorb or receive ink differently. The same print file can look brighter on one fabric and softer on another. Fabric construction, surface texture, moisture, pre-treatment, and finishing also influence final color. This is why color matching should always be tested on the actual production fabric, not only on a sample base that looks similar. Ink, Machine and Profile Must Work Together Color management depends on the relationship between ink, machine settings, RIP software, profiles, fabric, and production conditions. If one element changes, the color result may change. Manufacturers should maintain controlled settings for approved jobs and avoid unnecessary changes during repeat production. A stable workflow helps improve repeatability, especially for export orders, brand approvals, and bulk production. Sampling Helps Prevent Bulk Production Issues Sampling is an important part of color management. Before bulk production, manufacturers should print samples, review color output, check fabric behavior, and confirm customer approval. Once the sample is approved, the same settings and material combinations should be followed during production. This helps reduce shade variation and improves confidence between the printer and customer. Conclusion Color management in textile printing helps manufacturers control the journey from design screen to final fabric. It reduces shade variation, improves repeatability, and supports more reliable customer approvals. True Colors’ integrated model is especially useful for color-sensitive production because it connects multiple factors that affect final output. Machines, Inkia by True Colors inks, True Colors Sublimation Paper, fabrics, and technical support all influence color consistency in different ways. For manufacturers who struggle with repeated shade corrections, True Colors can help bring more structure to the printing process by supporting the complete production chain rather than focusing on one isolated component.
Commercial Inkjet for Book Printing and POD: Why Speed and Consistency Matter
The Publishing Industry Is Moving Towards Smarter Printing Book printing has changed significantly over the last few years. Publishers no longer want to print thousands of copies and store them in warehouses. Instead, they prefer flexible production that matches actual demand. This shift has made inkjet book printing an attractive option for publishers, educational institutions, self-publishing companies, and commercial print businesses. With digital production, books can be printed whenever they are needed, reducing unnecessary inventory and improving operational flexibility. As reader preferences and publishing schedules continue to evolve, print businesses also need production systems that can respond quickly without compromising quality. Why Print-on-Demand Is Growing Print-on-demand (POD) has become one of the biggest changes in the publishing industry. Rather than committing to large print runs, publishers can produce only the number of books they actually require. This approach offers several advantages. Inventory costs become lower, unsold books are reduced, and new titles can reach the market much faster. For commercial printers, POD also creates opportunities to handle multiple short-run jobs throughout the day. Instead of waiting for one large project, businesses can efficiently manage several smaller orders using digital workflows. As a result, production becomes more flexible and customer service improves. Speed Matters, but Quality Matters Even More Fast production is valuable only when every printed copy maintains the same quality. Readers expect sharp text, clean graphics, proper registration, and uniform print density from the first page to the last. Even small inconsistencies can affect the reading experience and reduce customer satisfaction. That is why inkjet book printing should always be evaluated on both productivity and print quality. A machine that prints quickly but creates rework or inconsistent output can increase production costs instead of reducing them. Reliable performance is what truly improves efficiency. Consistency Builds Long-Term Customer Confidence Many publishers reorder the same title several times throughout the year. Every new batch should closely match the previous one. Maintaining this consistency requires more than accurate machine settings. Paper quality, ink performance, operator practices, and workflow control must all work together throughout production. When every component performs consistently, printers can deliver repeat orders with greater confidence. This reliability strengthens customer relationships and encourages long-term business partnerships. Commercial Inkjet Opens New Business Opportunities Commercial inkjet technology is no longer limited to book production. The same systems can also support educational materials, training manuals, corporate reports, personalized publications, technical documentation, and many other short-run print applications. This flexibility allows print businesses to expand into new markets without completely changing their production process. As demand for customized and on-demand printing continues to grow, commercial inkjet technology gives businesses the ability to diversify their services while improving overall production efficiency. Conclusion Inkjet book printing is helping transform modern publishing by combining speed, flexibility, and production consistency. For commercial print businesses, it supports print-on-demand workflows, reduces inventory dependence, and makes it easier to manage multiple short-run projects without sacrificing quality. True Colors’ dedicated Commercial Inkjet Printing division is built to support this new generation of digital production. By combining advanced commercial inkjet technology with industry expertise and reliable technical support, True Colors helps print businesses build efficient, scalable, and future-ready printing operations that can confidently meet the changing demands of the publishing industry.
How Digital Printing Supports Small Batch and On-Demand Textile Production
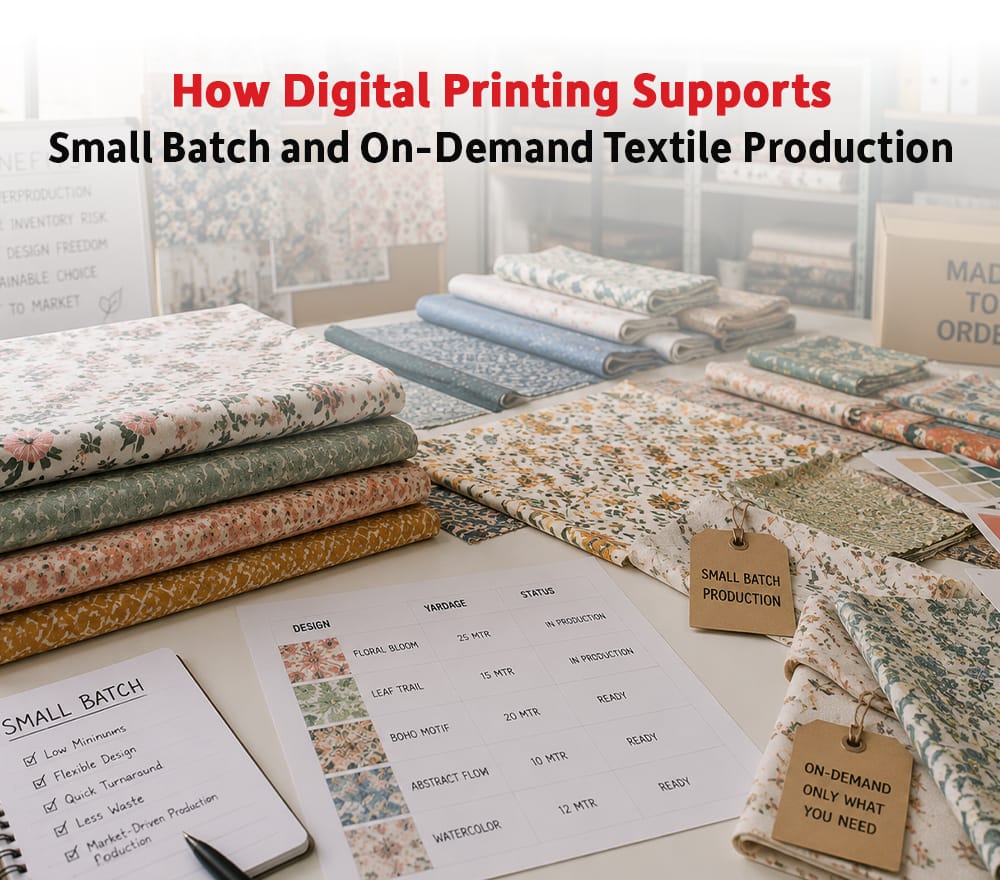
Textile Production Is Becoming More Flexible The textile industry is shifting from large fixed production to more flexible manufacturing models. Brands now want shorter runs, frequent design changes, customized products, and faster response to market demand. This is where on-demand textile printing becomes important. On-demand textile printing allows manufacturers to print based on actual requirement instead of producing large quantities in advance. Digital printing technology supports this model because it reduces setup time and makes design changes easier. For fashion brands, designers, e-commerce businesses, and boutique labels, this flexibility can create a major advantage. Small Batch Production Reduces Inventory Risk One of the biggest challenges in textile production is inventory risk. When brands produce large quantities before knowing customer demand, unsold stock can become a financial burden. On-demand textile printing helps reduce this risk by allowing smaller production batches. Brands can test designs, study demand, and then repeat only the products that perform well. Manufacturers who offer small batch digital printing can become valuable partners for brands that want to stay agile. Customization Becomes Easier Customers increasingly look for unique designs, limited editions, and personalized products. Digital printing supports customization because each design can be changed digitally without long setup processes. This allows printers to handle personalized patterns, special collections, regional designs, and niche product categories. For businesses serving online fashion, home décor, gifting, or designer fabrics, on-demand textile printing can support new revenue opportunities. Customization becomes more practical when production is flexible. Faster Sampling Supports Faster Launches On-demand production depends on fast sampling and quick approvals. Digital textile printing helps brands move from concept to sample faster. Once the design is approved, production can begin without major preparation delays. This is useful for seasonal fashion, festive collections, influencer-led merchandise, limited drops, and fast-moving retail launches. A faster sampling cycle helps brands remain relevant in changing markets. Production Control Still Matters Although on-demand textile printing supports flexibility, it still requires production discipline. Manufacturers must maintain consistent color, fabric quality, ink performance, and finishing standards even for small batches. Short-run production should not mean casual production. Every order must meet quality expectations, whether it is ten meters or ten thousand meters. To succeed in on-demand printing, businesses need a stable digital printing ecosystem. Conclusion On-demand textile printing supports small batches, faster launches, custom designs, and reduced inventory risk. It gives brands more flexibility and gives manufacturers new opportunities in short-run and personalized production. True Colors supports this shift by offering a digital printing ecosystem that can serve both growing manufacturers and flexible production businesses. With digital textile printing machines, Inkia by True Colors inks, True Colors Sublimation Paper, fabrics, and technical support, the brand helps printers manage quality even when order patterns keep changing. For businesses entering on-demand textile printing, True Colors can help build the foundation for flexible production without losing focus on consistency and reliability.
Sublimation Paper Storage Mistakes That Affect Transfer Printing Quality
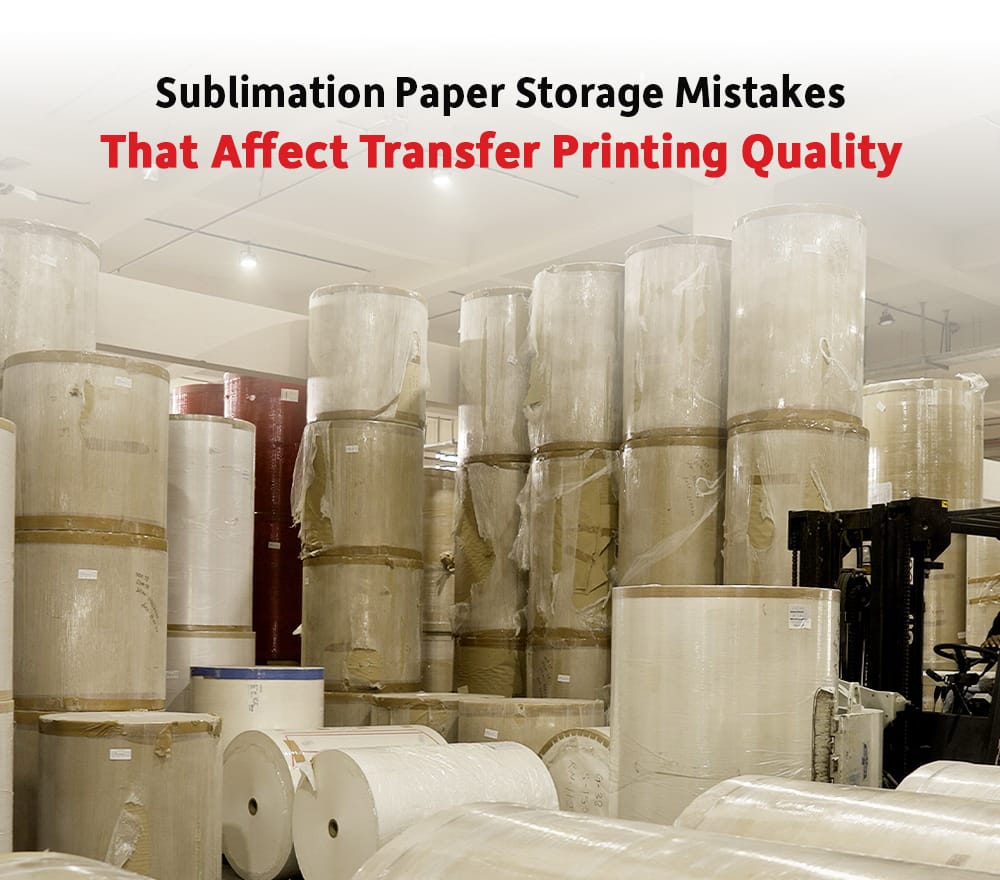
Good Paper Can Fail If Stored Incorrectly Sublimation paper plays a major role in transfer printing quality. It carries the printed image and releases the ink onto fabric during the heat transfer process. However, even good sublimation paper can create problems if it is not stored properly. Sublimation paper storage affects moisture level, flatness, ink behavior, drying, and transfer consistency. Many printers face paper-related issues without realizing that the problem may have started in storage, not during printing. For sublimation printers, proper paper handling is an important part of production discipline. Moisture Is One of the Biggest Risks Sublimation paper is sensitive to moisture. When paper absorbs moisture from the environment, it may curl, wrinkle, or behave unevenly during printing and transfer. Moisture can also affect how ink sits on the paper and how it releases during heat transfer. In humid conditions, printers may notice dull output, uneven transfer, slow drying, or paper movement issues. This is especially important in regions where seasonal humidity changes are common. During monsoon or high-humidity periods, paper storage needs extra attention. Heat and Direct Exposure Can Affect Paper Behavior Sublimation paper should not be exposed to direct sunlight, excessive heat, dust, or open factory conditions for long periods. Heat and exposure can disturb the paper’s coating behavior and handling quality. Dust can also create small defects during printing. Paper rolls should be stored in clean and controlled conditions. Once opened, they should be handled carefully and protected from moisture and contamination. Poor handling can create avoidable printing defects even when the printer and ink are working properly. Paper Curling Can Slow Down Production One common issue caused by poor sublimation paper storage is curling. Curled paper can affect feeding, alignment, printing smoothness, and transfer accuracy. It may also increase operator intervention and slow down production. In high-speed sublimation workflows, paper behavior must remain stable. If the paper does not move properly through the printer or transfer process, production efficiency suffers. This is why paper storage should be treated as a production requirement, not as a warehouse formality. Storage Discipline Improves Transfer Consistency Proper storage helps maintain paper performance from roll to roll. When sublimation paper is protected from moisture, dust, and temperature imbalance, it can support more predictable printing and transfer results. This improves color consistency, sharpness, drying behavior, and production flow. Printers who standardize storage practices can reduce unexplained defects and improve confidence during bulk jobs. Conclusion Sublimation paper storage directly affects transfer printing quality. Moisture, heat, dust, and poor handling can lead to curling, uneven transfer, slow drying, and production delays. For printers, good storage discipline is as important as choosing good sublimation paper. True Colors Sublimation Paper is designed to support reliable sublimation printing, but its best performance is achieved when it is used within the right production and storage conditions. True Colors strength lies in helping printers understand this full journey, from paper selection to actual transfer output. With support from the wider True Colors ecosystem, including inks, machines, fabrics, and technical guidance, sublimation printers can improve not only their paper choice but also the way paper performs in daily production.
Textile Print Sampling: Why Speed Matters for Product Development
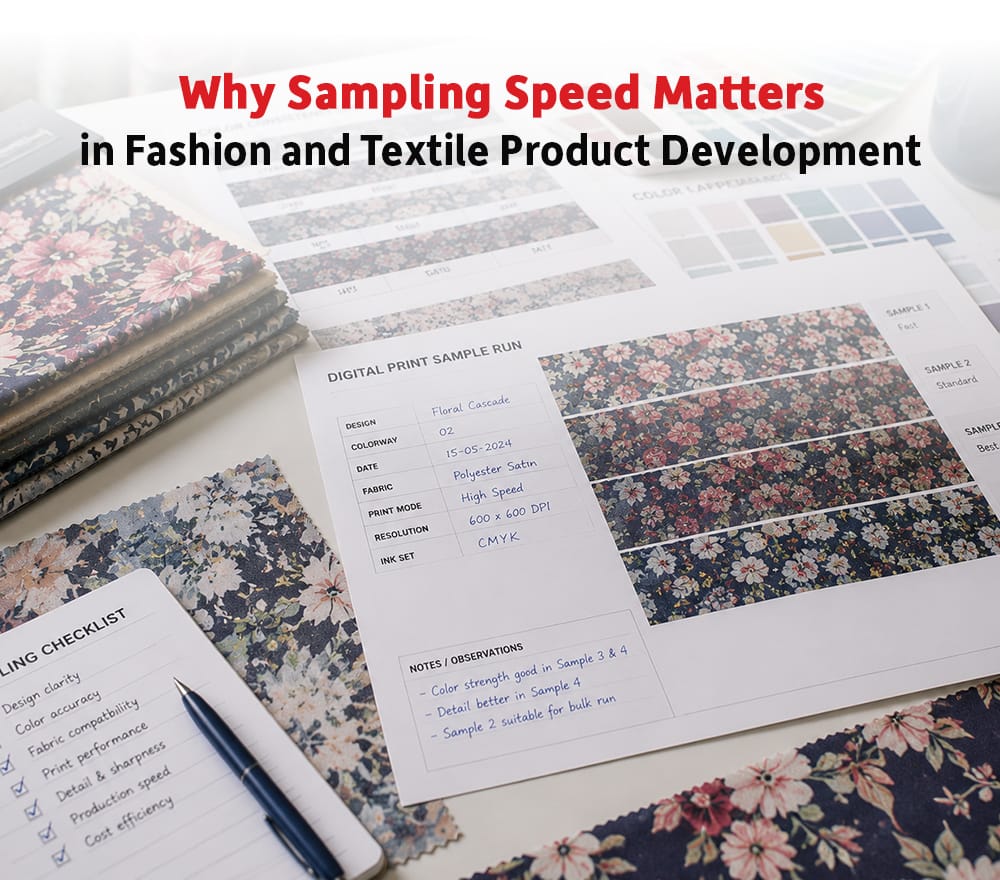
Sampling Decides How Fast a Collection Moves In fashion and textile product development, sampling is not a small step. It often decides how quickly a collection can move from idea to production. Brands need to test prints, colors, fabrics, scale, and product feel before placing larger orders. If sampling takes too long, the complete launch timeline gets delayed. This is why textile sampling with digital printing has become important for fashion brands, exporters, designers, and manufacturers. Digital printing allows businesses to create samples faster and with more design flexibility compared to processes that require longer setup. Faster Sampling Improves Decision-Making When brands receive samples quickly, they can make decisions faster. They can approve designs, change colorways, adjust scale, test fabrics, and finalize collections with less waiting time. This helps reduce the gap between design planning and production. In fast-moving fashion markets, this speed can become a competitive advantage. A delay of even a few days can affect seasonal launches, buyer approvals, or market timing. Digital textile printing helps reduce such delays by simplifying the sampling process. Multiple Design Options Can Be Tested Easily Fashion development often requires experimentation. A brand may want to see the same artwork in different colors, different scales, or different fabric bases. Digital printing makes it easier to test these variations without committing to large quantities. This helps designers and buyers compare options before finalizing production. Manufacturers also benefit because they can present more possibilities to customers and improve approval chances. The ability to test quickly can lead to better design confidence and fewer corrections during bulk production. Sampling Reduces Production Risk A well-executed sample helps identify problems before bulk printing begins. It allows the team to check color output, fabric behavior, design scale, repeat accuracy, hand feel, and finishing compatibility. If issues are found during sampling, they can be corrected before large quantities are printed. This helps reduce rejection, wastage, and buyer dissatisfaction. Digital textile sampling is therefore not only about speed. It is also about risk control. Repeatability Matters After Approval Once a sample is approved, the production team must be able to reproduce the same result in bulk. This requires stable ink, machine settings, fabric handling, color profiling, and process control. A fast sample is useful only when it can be converted into consistent production. Manufacturers should maintain proper records of approved settings and material combinations so that the final fabric matches the approved sample as closely as possible. Conclusion Textile sampling with digital printing helps fashion brands and manufacturers move faster, test more ideas, reduce risk, and improve production planning. In markets where trends change quickly, sampling speed can directly affect business opportunities. True Colors’ digital printing ecosystem is well suited for this need because it connects machines, inks, fabrics, sublimation paper, and technical support within one production understanding. For sampling-driven businesses, this helps reduce confusion between design expectations and production realities. By supporting both the creative and technical sides of textile printing, True Colors helps brands and manufacturers turn design ideas into production-ready fabrics with greater speed and confidence.
Industrial Textile Printers vs Entry-Level Machines: What Growing Businesses Should Compare
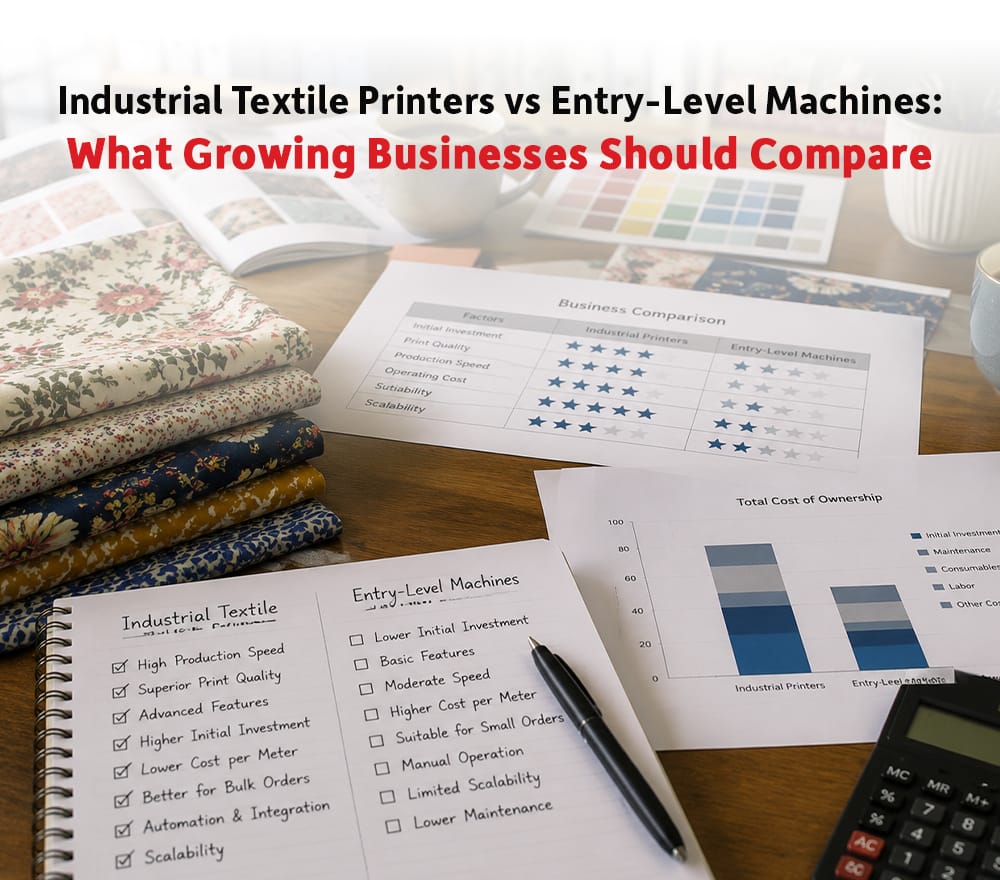
Growth Changes Machine Requirements Many textile businesses begin with entry-level digital printing machines. These systems are useful for learning, sampling, smaller jobs, and early-stage production. However, as order volume increases, the limitations of entry-level machines become more visible. A growing business may start facing longer production hours, slower delivery, limited fabric handling, quality variation, and higher operator dependency. At this stage, the discussion often shifts toward investing in an industrial textile printer. The decision should not be based only on machine size or speed. It should be based on production expectations, customer requirements, workflow maturity, and long-term business plans. Entry-Level Machines Have a Different Purpose Entry-level machines can be suitable for businesses that handle small quantities, design trials, boutique production, or limited applications. They usually require lower investment and may be easier to start with. For new businesses, this can be a practical first step. However, entry-level machines may not always support continuous high-volume production. Their speed, stability, fabric handling, ink system, and duty cycle may not match the requirements of industrial printing units. As a business grows, these limitations can affect production planning and profitability. Industrial Textile Printers Are Built for Production Pressure An industrial textile printer is designed for more serious production environments. It usually supports higher output, longer running hours, better stability, and more controlled fabric handling. For businesses serving fashion brands, export houses, large fabric orders, or continuous production, this becomes important. Industrial systems are expected to maintain better consistency across longer runs. This includes print alignment, ink flow, color stability, and fabric movement. When a machine becomes part of daily bulk production, reliability becomes as important as speed. Scalability Should Be a Major Decision Factor Growing businesses should not buy machines only for today’s workload. They should also consider future production needs. If order volume is expected to increase, the machine should support higher capacity, faster workflow, better operator control, and improved production planning. A machine that is suitable today but becomes restrictive within a short time may lead to another investment sooner than expected. The right industrial textile printer should support the business as it expands, not limit its next stage of growth. Service Support Becomes More Important with Industrial Production As machine capacity increases, downtime becomes more expensive. When an entry-level machine stops, the impact may be limited. But when an industrial textile printer is responsible for large daily output, downtime can affect delivery commitments and customer trust. This is why service support, spare parts availability, operator training, and preventive maintenance become critical. A growing business should choose not only the machine but also the technology partner behind it. Conclusion The choice between an industrial textile printer and an entry-level machine depends on production scale, quality expectations, uptime requirements, and growth plans. Entry-level machines may help businesses begin, but industrial systems are better suited for manufacturers who need reliability, consistency, and scalable output. True Colors supports growing textile businesses by helping them look beyond the first machine purchase. With experience in digital textile printing machines and a wider ecosystem that includes inks, sublimation paper, fabrics, and technical support, True Colors helps manufacturers evaluate machines based on real production requirements. For businesses preparing to move from small-scale printing to industrial production, True Colors can act as a technology partner that understands both the machine and the production environment around it.
How to Calculate Real Production Cost in Digital Textile Printing
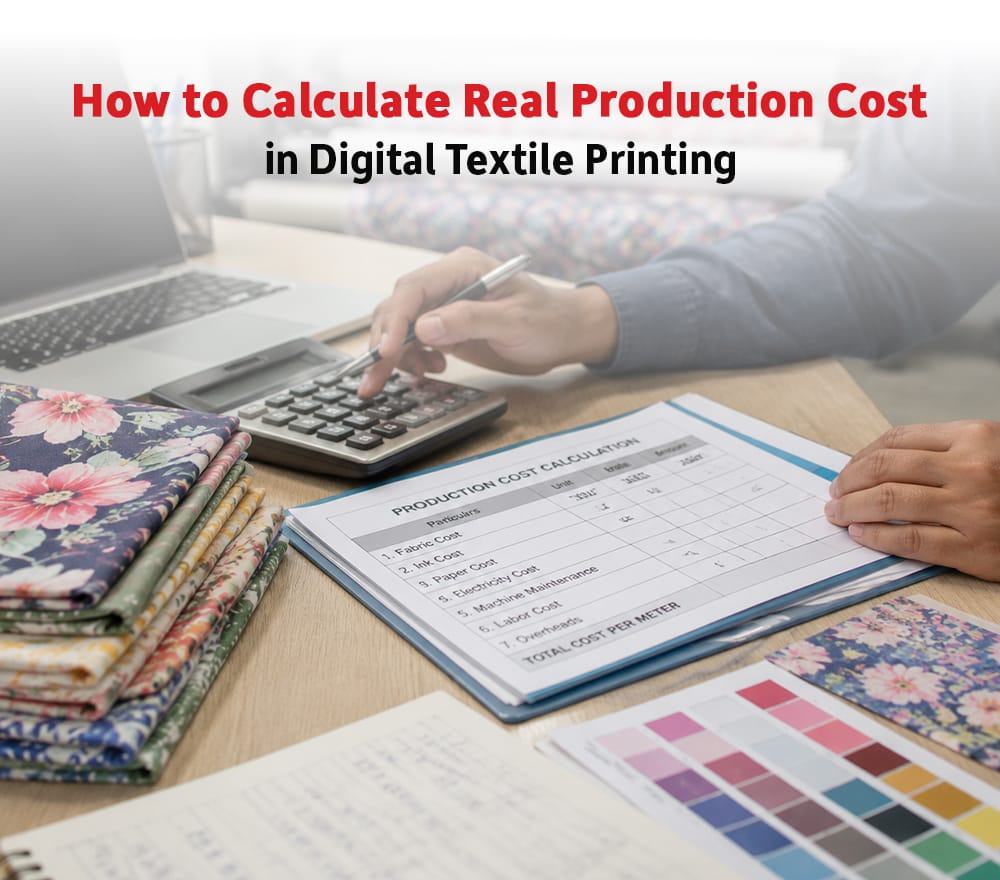
Print Cost Is More Than Ink Consumption Many textile printers calculate production cost by looking mainly at ink consumption and fabric cost. This gives an incomplete picture. Real digital textile printing cost calculation should include every factor that affects production output, quality, wastage, and delivery. A job that looks profitable on paper may become expensive if there is repeated sampling, high rejection, slow production speed, machine downtime, or poor material compatibility. For textile manufacturers, understanding real production cost is important for pricing, planning, and long-term profitability. Machine Time Has a Cost Every hour of machine operation has a value. When a machine is used for printing, sampling, cleaning, reprinting, or waiting due to avoidable delays, it affects the overall cost of production. A high-speed digital textile printing machine may reduce cost per meter when it runs efficiently. However, speed alone does not guarantee lower cost if the workflow is unstable. Manufacturers should consider how much usable output the machine produces in a day, not only the maximum speed mentioned in specifications. Actual productivity depends on design changes, fabric loading, ink behavior, operator skill, maintenance routine, and order planning. Consumables Influence Final Cost Ink, sublimation paper, fabric, pre-treatment chemicals, finishing inputs, and packaging all influence production cost. Poor-quality consumables can increase hidden expenses. For example, low-cost paper may lead to transfer defects, unstable ink may increase cleaning cycles, and unsuitable fabric may create more rejection. When manufacturers calculate cost, they should consider how consumables perform during real production. The cheapest input is not always the most cost-effective input. A slightly better consumable can sometimes reduce reprinting, wastage, downtime, and customer complaints. Wastage Changes the True Cost Per Meter Fabric wastage can completely change cost calculation. If a job requires extra printing because of shade variation, file errors, fabric movement, nozzle issues, or transfer defects, the final cost per meter increases. Many manufacturers forget to include rejection percentage while pricing a job. This creates pressure later when actual production losses appear. A realistic cost calculation should include expected wastage based on fabric type, design complexity, production method, and operator experience. Reducing wastage is one of the most effective ways to improve profitability in digital textile printing. Service and Maintenance Should Be Included Maintenance is often treated as a separate expense, but it directly affects production cost. Machines that are not maintained properly may consume more time, create more defects, and face more downtime. Spare parts, technical service, cleaning materials, and preventive maintenance should be considered as part of the real cost structure. A strong service system can reduce emergency breakdowns and improve machine availability. This makes the overall production cost more predictable. Conclusion Digital textile printing cost calculation should go beyond ink and fabric. Real cost includes machine time, consumables, wastage, labor, maintenance, downtime, sampling, and production efficiency. For textile businesses, better cost understanding leads to better pricing and healthier margins. True Colors can support manufacturers in this area because its offering is not limited to one part of the production chain. With digital textile printing machines, Inkia by True Colors inks, True Colors Sublimation Paper, fabrics, and service support, businesses can evaluate cost through an integrated production lens. Instead of calculating each input separately without understanding its production impact, manufacturers can work with True Colors to build a more stable and predictable printing ecosystem. This helps improve not only output quality but also cost control across daily operations.
Digital Printing for Home Textiles: Curtains, Cushions, Bedsheets and More
Home Textiles Need Design Variety Home textiles are no longer limited to basic prints and standard patterns. Customers now look for coordinated themes, seasonal designs, personalized décor, premium prints, and faster availability across multiple product categories. This has made digital printing for home textiles more important for manufacturers, brands, and exporters. Products such as curtains, cushions, bedsheets, table covers, blinds, décor fabrics, and soft furnishing materials require strong design flexibility. Digital textile printing helps manufacturers create multiple patterns, color options, and design collections without depending on long setup processes. For home textile businesses, this flexibility can improve collection planning and help respond faster to market demand. Why Digital Printing Works Well for Home Furnishing Fabrics Home textile products often require large design repeats, detailed artwork, soft color transitions, and theme-based collections. Digital printing supports these needs because it allows direct reproduction of complex artwork on fabric. Unlike traditional processes where each design may require more setup time, digital printing makes it easier to produce different designs in shorter runs. This is useful for businesses that want to test new collections, produce boutique home décor ranges, or create customized furnishing fabrics. For manufacturers supplying to décor brands or export houses, digital printing can help reduce design limitations and improve product variety. Fabric Selection Plays an Important Role The final result in home textile printing depends heavily on fabric selection. Polyester, cotton, blends, viscose, and other materials behave differently during printing and finishing. For certain polyester-based home textile applications, sublimation printing can deliver bright and clean output. For natural fabrics, other printing methods may be more suitable depending on the product use and performance requirement. A curtain fabric may need different print behavior compared to a cushion cover or bedsheet. The fabric feel, color strength, washing requirement, light exposure, and finishing process should all be considered before selecting the printing method. Digital printing gives flexibility, but the right fabric and ink combination decide the final quality. Consistency Is Important Across Matching Products Home textile collections often include multiple matching products. A single design theme may be used across curtains, cushion covers, bedsheets, and table linen. This makes color consistency very important. If the shade changes from one product to another, the collection may lose its visual balance. Manufacturers need proper color management, stable inks, controlled fabric handling, and repeatable production settings. Digital printing can support coordinated collections, but only when the production process is managed carefully. Faster Sampling Helps Brands Launch More Collections Home décor trends change with seasons, festivals, interior themes, and customer preferences. Brands often need to create new collections quickly. Digital textile printing helps speed up sampling because new designs can be tested without long preparation time. Manufacturers can present more options to buyers, finalize designs faster, and move into production with greater confidence. This allows home textile brands to stay fresh in the market and offer more variety to customers. Conclusion Digital printing for home textiles supports design variety, faster sampling, coordinated collections, and flexible production across curtains, cushions, bedsheets, table covers, and décor fabrics. For manufacturers, it opens opportunities to serve both bulk and customized home furnishing markets with more agility. True Colors’ sublimation paper division is especially relevant for polyester-based home textile applications where transfer quality, clean output, and repeatable color release matter. Along with True Colors Sublimation Paper, the brand’s wider ecosystem of digital printing machines, Inkia by True Colors inks, fabrics, and technical support gives manufacturers a stronger base for home textile production. For businesses building furnishing collections, True Colors can support the journey from print planning to production stability, helping manufacturers deliver home textile products with better consistency and market readiness.
Why Ink Stability Matters in Long-Run Digital Textile Printing
Stable Ink Creates Stable Production In digital textile printing, ink is often discussed only in terms of color strength and price. Many manufacturers compare inks based on shade, vibrancy, or cost per litre. While these factors matter, they do not show the complete picture. For production units that run machines for long hours, ink stability becomes one of the most important factors in daily printing performance. Ink stability in digital textile printing refers to how consistently the ink behaves during storage, circulation, printing, and long production runs. A stable ink should maintain proper flow, color behavior, viscosity, and print performance over time. When ink remains stable, the machine can run with fewer interruptions and the printed fabric can maintain more predictable quality. Long-Run Printing Reveals Ink Performance Short sampling runs rarely expose the full behavior of an ink. A print may look good during a trial, but the real test begins when the machine runs continuously for several hours. During long-run production, unstable ink may create issues such as shade variation, weak flow, nozzle disturbance, inconsistent droplet formation, or print defects. These issues may not appear immediately, but they can gradually affect output quality as the production continues. For textile manufacturers handling bulk orders, this becomes a serious concern. Even a small change in color or print sharpness across a long order can lead to rejection, reprinting, and loss of production time. This is why ink selection should be based on production reliability and not only on the first sample result. Ink Stability Protects Printheads Printheads are one of the most sensitive and valuable components in a digital textile printing machine. Their performance depends heavily on ink quality, filtration, flow behavior, and machine maintenance. If the ink does not remain stable, it can increase the risk of nozzle clogging, uneven firing, and flow-related problems. These issues can affect print quality and may also increase maintenance pressure on the production team. Stable ink supports smoother movement through the system and helps maintain more consistent printhead performance during daily production. It also reduces unnecessary cleaning cycles, which can save time and improve machine availability. For manufacturers, this means ink stability is not just a quality issue. It is also connected to machine health and long-term production cost. Color Consistency Depends on Ink Behavior In textile printing, color consistency is a major requirement, especially for bulk fabric orders, export production, fashion repeats, and brand-approved shades. When ink behavior changes during production, the final fabric may show visible shade differences. This can become a major challenge when a customer expects the same design to match across different lots. Ink stability helps reduce such variation by maintaining predictable color behavior across production cycles. The machine settings, fabric type, environmental conditions, and ink profile all play a role, but the ink itself must remain dependable. A good digital textile printing setup should therefore consider ink as part of the complete production system, not as a standalone consumable. Storage and Handling Also Matter Even good-quality ink can perform poorly if it is not stored or handled properly. Temperature, dust, contamination, exposure, and poor handling practices can affect ink behavior before it reaches the machine. Manufacturers should maintain clean storage conditions and ensure that operators follow proper ink handling discipline. The goal should be to protect the ink from unnecessary instability and maintain its expected performance throughout production. Ink stability is built through both product quality and production discipline. When both work together, manufacturers can achieve better print reliability. Conclusion Ink stability in digital textile printing directly affects long-run performance, printhead reliability, color consistency, and production confidence. For manufacturers who print continuously, the right ink can help reduce interruptions, avoid repeated corrections, and support more predictable fabric output. This is where Inkia by True Colors becomes relevant for textile printers looking at production-focused ink performance. Instead of treating ink as only a consumable, True Colors connects ink with the larger printing ecosystem of machines, fabrics, sublimation paper, and service support. This helps manufacturers evaluate ink in the way it actually performs on the production floor. For businesses running long production cycles, True Colors’ ecosystem approach allows better coordination between machine performance, ink behavior, and technical support. This makes ink selection a more reliable production decision rather than a trial-and-error activity.