Pigment Printing in 2026: Why Brands Are Looking at Simpler Textile Workflows
Textile Brands Want Simpler Production Textile brands are under pressure to launch faster, reduce development delays, control inventory, and offer more design variety. This has increased interest in printing methods that can simplify production workflows. Pigment printing in textile production is often discussed because it can support a simpler process for many applications compared to some traditional dye-based workflows. For brands and manufacturers, the appeal of pigment printing lies in its ability to support flexible design production with potentially fewer process complications, depending on the fabric, ink system, curing method, and final performance requirement. Why Pigment Printing Is Gaining Attention Pigment printing is used on different textile materials, especially where brands want design flexibility and process efficiency. Unlike some printing methods that require more intensive washing or steaming steps, pigment printing can be attractive for manufacturers looking at simpler production routes. However, it still requires proper process control, correct curing, suitable binder performance, and the right fabric selection. The main point is that pigment printing is not automatically simple by default. It becomes efficient when the full workflow is planned correctly. Fabric Feel and Fastness Must Be Managed One of the key factors in pigment printing is fabric feel. Since pigment color generally stays on the fabric surface with the help of binders, the final hand feel depends on the quality of the ink system, binder chemistry, curing, and fabric base. Brands should not judge pigment printing only by speed. They should also consider rubbing fastness, washing performance, color brightness, softness, and product application. For fashion fabrics, the print must not only look good but also feel acceptable to the customer. For home textiles or utility fabrics, performance requirements may be different. Pigment Printing Can Support Shorter Runs Modern textile brands often need smaller collections, quick sampling, and faster design changes. Pigment printing can support these needs when used with digital textile printing systems. It allows manufacturers to work with changing artwork and shorter production batches more easily than many traditional large-run processes. This can be useful for fashion labels, home textile brands, start-up designers, and businesses that want to test market response before producing larger quantities. Production Discipline Remains Important Even if pigment printing offers workflow advantages, production discipline is still essential. Manufacturers must control fabric preparation, ink performance, curing temperature, machine settings, and finishing quality. If the process is not stable, the final fabric may show poor durability, uneven color, or unacceptable texture. Pigment printing should therefore be approached as a structured production method rather than only a faster option. Conclusion Pigment printing textile workflows are gaining attention because brands want faster, simpler, and more flexible production. When planned properly, pigment printing can support shorter runs, design variety, and efficient textile manufacturing. True Colors can support manufacturers exploring pigment printing by helping them understand the relationship between machine technology, ink performance, fabric selection, and service support. With Inkia by True Colors inks, digital printing machines, fabrics, sublimation paper, and technical guidance, True Colors gives businesses a broader ecosystem for making better production decisions. For brands looking at simpler textile workflows, True Colors can help ensure that speed does not come at the cost of consistency, quality, or long-term reliability.
How to Plan Machine Capacity for Peak Textile Printing Season
Peak Season Tests Real Production Capacity Every textile manufacturer knows that peak season creates pressure. Orders increase, timelines become shorter, customer expectations rise, and machines run for longer hours. This is when textile printing machine capacity planning becomes very important. Many businesses calculate capacity based only on machine speed. However, real production capacity depends on usable output, machine uptime, job changeovers, fabric handling, maintenance, operator skill, ink stability, and finishing time. A machine may have a strong rated speed, but peak season success depends on how much consistent production the factory can actually deliver. Rated Speed Is Not the Same as Daily Output Machine brochures often mention maximum speed, but production floors operate under real conditions. During actual printing, time is spent on loading fabric, checking files, approving samples, cleaning printheads, changing rolls, adjusting settings, monitoring quality, and handling unexpected stoppages. This means the daily output may be lower than the theoretical machine speed. Manufacturers should plan capacity based on practical production numbers, not ideal conditions. This helps avoid overcommitting to customers and reduces delivery pressure. Order Mix Affects Capacity Peak season capacity also depends on the type of orders being printed. A factory handling one long repeat order may produce more meters in a day compared to a factory handling many short jobs with frequent design changes. Design complexity, ink coverage, fabric width, print quality requirement, sampling approvals, and finishing needs all influence actual capacity. This is why capacity planning should consider the full order mix rather than only the total number of meters required. Downtime Must Be Planned Before It Happens Many businesses think about downtime only when a machine stops. During peak season, this can become costly. Preventive maintenance should be planned before the rush begins. Operators should check machine health, ink systems, fabric feeding, printhead condition, software settings, and service requirements before production pressure increases. A well-maintained machine is more likely to support stable production during long working hours. People and Workflow Decide Final Capacity Machine capacity is not decided by the machine alone. Operators, supervisors, designers, quality teams, and finishing teams all affect output. If design files are delayed, fabric is not ready, operators are not trained, or finishing is overloaded, the printing machine cannot deliver its full potential. Peak season planning should therefore include the complete workflow from order confirmation to dispatch. When every department is aligned, production becomes smoother and more predictable. Conclusion Textile printing machine capacity planning helps manufacturers manage peak season pressure with more confidence. Real capacity depends on practical output, order mix, machine uptime, operator skill, maintenance, and workflow coordination. True Colors supports peak-season readiness by helping manufacturers look at production capacity as a complete system. Through digital textile printing machines, Inkia by True Colors inks, True Colors Sublimation Paper, fabrics, and technical service support, True Colors helps businesses prepare for high-demand periods with better stability. For manufacturers facing seasonal production pressure, True Colors can provide the machine knowledge, consumable understanding, and service support needed to keep printing operations more dependable when demand is at its highest.
Sublimation Printing for Advertising: Flags, Banners, Soft Signage and Display Fabrics
Advertising Needs High-Impact Printed Fabrics Advertising and promotional displays rely heavily on visual impact. Whether it is a flag, banner, exhibition backdrop, soft signage, retail display, or event fabric, the print must catch attention quickly. Sublimation printing for advertising is widely used for polyester-based display fabrics because it can deliver bright colors, sharp designs, and smooth transfer results. For print businesses and textile manufacturers, this creates opportunities in promotional graphics, event branding, retail displays, and outdoor or indoor advertising textiles. Why Sublimation Works for Display Fabrics Sublimation printing transfers dye into polyester fabric using heat. This makes it suitable for many advertising fabrics where color vibrancy and lightweight handling are important. Soft signage and fabric displays are popular because they are easier to transport, fold, install, and reuse compared to some rigid display materials. For businesses producing flags, banners, and display fabrics, sublimation printing can support detailed graphics and strong visual output. Color Strength Matters in Advertising Advertising graphics must be visible and memorable. Weak colors or dull prints can reduce the impact of a campaign. In sublimation printing, color strength depends on the ink, sublimation paper, fabric quality, heat transfer process, and production settings. If the transfer process is not controlled properly, the final output may look faded, uneven, or unclear. This is why print businesses serving advertising clients need reliable materials and consistent production practices. Fabric Movement and Finishing Are Important Display fabrics are often viewed from a distance, but this does not mean quality can be ignored. Poor alignment, wrinkles, stains, or uneven transfer can be visible in large-format graphics. For flags and banners, fabric movement, wind exposure, stitching, and finishing also influence final performance. The printing process should be planned with the final application in mind. A fabric used for an indoor exhibition backdrop may have different requirements compared to an outdoor flag. Advertising Printing Needs Fast Turnaround Many advertising jobs are urgent. Events, product launches, exhibitions, campaigns, and retail promotions often work on fixed deadlines. Sublimation printing supports faster production when the workflow is planned well. Digital design changes, roll-to-roll printing, transfer consistency, and efficient finishing can help businesses complete urgent jobs more confidently. For print businesses, speed and reliability are both important in advertising applications. Conclusion Sublimation printing for advertising supports flags, banners, soft signage, display fabrics, exhibition graphics, and promotional textile applications. It gives businesses the ability to create bright, lightweight, and visually strong printed fabrics for brand communication. True Colors Sublimation Paper is especially relevant for this segment because advertising fabrics require dependable transfer quality and consistent color release. Along with Inkia by True Colors inks, digital printing machines, fabrics, and technical support, True Colors helps print businesses create a more stable sublimation workflow. For companies producing promotional textiles and soft signage, True Colors can support the balance between speed, visual impact, and production consistency.
How to Identify the Right Textile Ink for Your Production Environment
Ink Selection Should Match the Production Floor Choosing textile ink is not only about selecting a colorant. It is a production decision that affects machine performance, fabric quality, printhead safety, color consistency, and long-term cost. The right textile ink for production printing depends on the actual environment in which the machine operates. A printer working with polyester fabric may need a different ink system compared to a manufacturer printing on cotton or blended fabrics. A business running long production hours may require stronger ink stability than a unit focused mainly on sampling. This is why ink selection should begin with production reality, not only with price comparison. Fabric Type Guides Ink Choice Fabric type is one of the first factors to consider when choosing textile ink. Polyester, cotton, viscose, silk, nylon, and blended fabrics respond differently to different ink systems. Sublimation ink is commonly used for polyester-based printing, while pigment, reactive, disperse, or other ink systems may be selected depending on the fabric and process requirement. If the ink does not match the fabric, the final output may show weak color, poor fastness, dull print, or uneven results. A good production setup begins with understanding the relationship between fabric and ink. Machine and Printhead Compatibility Matter Ink must also be compatible with the digital printing machine and printhead technology. Incorrect ink selection can affect flow behavior, nozzle performance, droplet formation, and maintenance frequency. It may also increase the risk of print defects or machine interruptions. Manufacturers should ensure that the ink is suitable for the machine system, printing speed, printhead type, filtration requirement, and circulation behavior. In production printing, compatibility is not optional. It directly affects machine uptime and output reliability. Production Environment Affects Ink Behavior The same ink can behave differently in different factory conditions. Temperature, humidity, dust, storage practices, operator handling, and machine maintenance can influence ink performance. If the environment is unstable, the printer may face more nozzle issues, shade variation, or inconsistent flow. Manufacturers should choose ink that performs reliably in their production conditions and also maintain proper storage and handling practices. Ink quality and production discipline must work together. Cost Should Be Measured Through Output Many businesses compare ink only by litre price. This can be misleading. A lower-priced ink may become expensive if it increases wastage, cleaning cycles, machine stoppage, rejection, or color correction. The better way to evaluate ink is by looking at final production output, consistency, machine safety, and rejection rate. In textile printing, the right ink is the one that helps the entire production system perform better. Conclusion Choosing textile ink for production printing requires understanding fabric type, machine compatibility, printhead safety, production environment, color requirement, and long-term cost. The right ink should support both print quality and operational reliability. Inkia by True Colors is positioned for printers who need ink solutions that connect with real production needs. With the wider support of True Colors digital printing machines, sublimation paper, fabrics, and technical guidance, ink selection becomes part of a complete production conversation. For manufacturers who want fewer surprises on the shop floor, True Colors helps connect ink performance with machine behavior and fabric output, making the printing process more dependable.
Digital Textile Printing for Export Markets: Quality Parameters Buyers Care About
Export Buyers Look Beyond Print Appearance Export markets demand consistency, reliability, and production discipline. A printed fabric may look attractive at first glance, but export buyers usually evaluate much more than design appearance. Export quality digital textile printing must meet expectations related to color accuracy, fabric performance, repeat consistency, finishing quality, packing, and delivery timelines. For manufacturers and export houses, this means the printing process must be controlled from artwork preparation to final inspection. Color Consistency Builds Buyer Confidence One of the most important quality parameters in export fabric printing is color consistency. Buyers expect approved samples and bulk production to match closely. If the shade changes between lots, the order may face rejection or claim issues. Color consistency depends on controlled file preparation, ink stability, machine settings, fabric quality, environmental conditions, and finishing process. Export-focused manufacturers must maintain proper records and repeatable production settings to reduce shade variation. Print Sharpness and Design Accuracy Matter Export buyers often work with detailed designs, brand-specific artwork, and strict approval processes. The final printed fabric should maintain motif clarity, repeat accuracy, scale correctness, and clean edges. Blurred prints, broken repeats, alignment problems, or unclear detailing can affect buyer approval. Digital textile printing can support high-detail designs, but only when file preparation, machine control, fabric handling, and ink behavior are properly managed. Fabric Performance Is Part of Print Quality Export buyers do not judge printed fabric only by how it looks. They also care about how it performs. Depending on the product, buyers may check washing behavior, rubbing performance, hand feel, shrinkage, color durability, and finishing quality. The print should remain suitable for the intended use, whether it is fashion apparel, home textiles, scarves, sportswear, or décor fabrics. This is why the printing method, ink system, fabric selection, and post-processing must be aligned with the final application. Timely Delivery Is Also a Quality Parameter In export production, late delivery can damage business relationships even if the fabric quality is good. Buyers work with launch calendars, shipping schedules, retail timelines, and seasonal commitments. A reliable digital printing partner must have strong production planning, machine uptime, service support, and communication discipline. Export quality is therefore not only technical. It also includes dependability. Conclusion Export quality digital textile printing requires color consistency, sharp output, fabric performance, finishing control, and reliable delivery. Export buyers care about the complete production experience, not just the printed design. True Colors can support export-focused businesses by bringing together the key elements that affect printed fabric quality. With digital textile printing machines, Inkia by True Colors inks, True Colors Sublimation Paper, fabrics, and service support, True Colors helps manufacturers build more controlled production systems. For export houses and manufacturers serving international buyers, True Colors can help strengthen the printing foundation needed for consistency, repeatability, and long-term buyer confidence.
Commercial Inkjet vs Offset Printing: Where Digital Print Production Makes Sense
Print Production Is No Longer One-Format For many years, offset printing has been a strong choice for large-volume print production. It is known for quality, efficiency at scale, and wide use across commercial printing applications. However, customer requirements are changing. Print buyers now ask for shorter runs, faster turnaround, personalized content, and more flexible ordering. This is why the comparison of commercial inkjet vs offset printing has become important for print businesses. The goal is not to say one method is always better than the other. The goal is to understand where each method makes sense. Offset Printing Works Well for Long Runs Offset printing can be highly effective when the job volume is large, the design is fixed, and the production requirement is stable. For standard long-run jobs, offset can offer strong consistency and cost efficiency after setup. However, offset printing usually involves plates, setup time, and longer preparation. This may not always suit jobs where quantities are small, content changes frequently, or delivery timelines are very short. For such work, digital print production can offer more flexibility. Commercial Inkjet Supports Flexible Production Commercial inkjet printing is useful where print businesses need speed, shorter runs, quick job changeovers, and variable data capability. It allows printers to handle changing content without traditional setup limitations. This is useful for print-on-demand, book printing, transactional printing, direct mail, personalized communication, educational material, and short-run commercial jobs. In markets where customers want faster and more customized print, commercial inkjet can help businesses respond better. Personalization Is a Major Difference One of the biggest advantages of commercial inkjet printing is personalization. Each printed piece can carry different names, addresses, codes, images, offers, or content. This is difficult to manage efficiently with conventional fixed-print methods. As marketing and communication become more targeted, variable data printing is becoming more valuable. Commercial inkjet gives print businesses the ability to serve these modern requirements. The Best Choice Depends on the Job Print businesses should not choose technology based on trend alone. The right choice depends on job quantity, turnaround time, content variation, quality requirement, paper type, finishing process, and customer expectation. Offset may remain suitable for certain large-volume fixed jobs. Commercial inkjet may be better for flexible, fast, personalized, and short-run production. Many modern print businesses may need both approaches for different job categories. Conclusion Commercial inkjet vs offset printing is not about replacing one method completely. It is about understanding where digital print production makes better business sense. Commercial inkjet is especially useful for short runs, personalization, faster turnaround, and flexible production. True Colors Commercial Inkjet Printing division is relevant for print businesses exploring this shift. With digital printing experience and a production-focused approach, True Colors helps businesses look at commercial inkjet as a growth opportunity rather than only a technology upgrade. For printers evaluating the next stage of expansion, True Colors can support the move toward faster, smarter, and more flexible digital print production.
Why Textile Manufacturers Need a Complete Printing Ecosystem, Not Just a Machine
A Machine Alone Cannot Deliver Reliable Production Many textile manufacturers begin their digital printing journey by comparing machine speed, print width, printhead configuration, price, and technical specifications. Although these factors are important, they do not guarantee reliable production on their own. In reality, a textile printing ecosystem has a much greater impact on daily operations than the machine alone. Every stage of production is connected. Machines, inks, fabrics, sublimation paper, software, operators, service support, and the production environment all influence the final result. Therefore, if one part of the system performs poorly, the entire production process can slow down or produce inconsistent output. Every Part of the Process Works Together Digital textile printing is not an isolated activity. Instead, every production component affects the next one. For example, a high-performance machine cannot produce excellent results if the ink lacks stability, the fabric is unsuitable, or the sublimation paper fails to transfer ink properly. Likewise, even premium consumables cannot deliver consistent quality when the machine is poorly maintained or operators follow inconsistent practices. For this reason, manufacturers should build a production setup where every component works together instead of treating each element separately. Reliable Service Support Keeps Production Running Many businesses think about after-sales service only after a machine develops a problem. However, reliable support should become part of the production strategy from the very beginning. Fast technical assistance, preventive maintenance, operator training, spare parts availability, and troubleshooting all help reduce downtime. As a result, production remains stable even during large orders or peak manufacturing periods. Most importantly, strong service support gives manufacturers greater confidence when customer deadlines become tighter. Consumables Influence More Than Running Costs Many manufacturers purchase inks, sublimation paper, and fabrics by comparing prices alone. However, consumables influence much more than the monthly operating budget. The right materials improve color consistency, transfer quality, machine performance, and production reliability. On the other hand, incompatible consumables often increase wastage, maintenance requirements, print defects, and customer complaints. Therefore, businesses should evaluate consumables based on overall production performance rather than only their purchase cost. Growing Businesses Need an Integrated System As production expands, operations naturally become more complex. More customers, more designs, different fabric types, additional operators, and shorter delivery timelines all increase production pressure. Because of this, manufacturers need more than a high-speed machine. They also need a complete system that connects workflow, consumables, maintenance, technical support, and quality control. An integrated textile printing ecosystem makes it easier to standardize production, reduce unexpected issues, and scale operations with greater confidence. Conclusion A reliable textile printing ecosystem gives manufacturers much more than advanced equipment. It creates a connected production environment where machines, inks, sublimation paper, fabrics, software, operators, and technical support work together to deliver consistent results. This is exactly the approach followed by True Colors. Instead of supplying only a digital textile printing machine, True Colors provides a complete ecosystem that includes digital textile printing machines, Inkia by True Colors inks, True Colors Sublimation Paper, fabrics, and the expert support of TRUE TEAM. As a result, manufacturers can solve production challenges through one coordinated system instead of managing machine, ink, paper, and fabric issues separately. This integrated approach helps businesses improve consistency, increase efficiency, and build a stronger foundation for long-term growth.
Digital Printing in India’s Textile Industry: What Will Define the Next Phase of Growth
India’s Textile Industry Is Ready for Its Next Transformation India has built one of the world’s largest textile industries. From fabric manufacturing and processing to apparel, home textiles, and exports, the country has developed a strong production ecosystem over several decades. Today, however, the industry is entering a different phase. Customer expectations are changing faster than ever. Brands demand quicker product launches, buyers expect consistent quality, and manufacturers must balance efficiency with flexibility. As a result, India textile printing is no longer evolving only through faster machines. The next stage of growth will depend on how well manufacturers combine technology, production planning, quality control, and customer responsiveness. Faster Production Is Becoming a Business Requirement Modern textile markets move much faster than they did a few years ago. Fashion collections change frequently, export buyers work with tighter schedules, and retailers expect shorter delivery cycles. Because of this, manufacturers cannot depend on long production setups anymore. Digital textile printing allows businesses to move from design approval to production much more quickly while reducing unnecessary delays. However, speed alone is not enough. Manufacturers must maintain the same quality standards even when production volumes increase. Businesses that successfully combine speed with consistency will have a stronger competitive position. Customization Is Creating New Opportunities Today’s customers want products that feel unique. Limited collections, regional designs, seasonal launches, and personalized textiles are becoming increasingly common across fashion and home décor markets. Digital printing supports this shift because manufacturers can change artwork quickly without extensive setup procedures. Consequently, businesses can experiment with new ideas, launch smaller collections, and respond to customer demand with much greater confidence. Instead of producing large quantities first and hoping they sell, brands can test the market and expand production only after receiving positive customer response. Sustainable Manufacturing Will Become More Important Sustainability is no longer just a marketing term. Many brands now evaluate how fabrics are produced before selecting manufacturing partners. Digital textile printing can contribute to more responsible production by supporting shorter runs, reducing unnecessary inventory, and simplifying sampling. Nevertheless, sustainability involves much more than printing technology alone. Fabric selection, ink systems, energy consumption, production efficiency, and waste management all influence the environmental impact of textile manufacturing. Therefore, future-ready manufacturers will focus on improving the entire production process rather than one individual stage. Export Markets Will Continue to Raise Quality Standards Indian textile manufacturers serve customers across the world. International buyers expect accurate color matching, consistent fabric quality, reliable finishing, and timely deliveries on every order. Meeting these expectations requires more than advanced equipment. Manufacturers need standardized workflows, disciplined production practices, skilled operators, and dependable quality control systems. Companies that consistently deliver reliable results will strengthen buyer confidence and create stronger long-term export relationships. Connected Production Systems Will Shape the Future As production becomes more complex, managing individual components separately becomes increasingly difficult. Machines, inks, fabrics, sublimation paper, software, operators, technical support, and production planning all influence one another. When these elements work together, manufacturers experience fewer interruptions, better consistency, and smoother operations. For this reason, the future of India textile printing will belong to businesses that invest in complete production ecosystems instead of isolated technologies. Conclusion The next chapter of India textile printing will not be defined only by faster machines. It will be shaped by manufacturers who combine flexibility, customization, sustainability, quality control, and integrated production into one efficient workflow. True Colors is helping businesses prepare for this transformation through a complete digital printing ecosystem. Along with digital textile printing machines, the company offers Inkia by True Colors inks, True Colors Sublimation Paper, fabrics, commercial inkjet solutions, and the technical expertise of TRUE TEAM. By connecting every stage of production, True Colors enables manufacturers to build operations that are more reliable, scalable, and ready for the future of India’s textile industry.
How Textile Brands Can Use Digital Printing for Limited Edition Collections
Limited Edition Collections Need Flexible Production Textile and fashion brands are increasingly using limited edition collections to create exclusivity and market excitement. These collections may be seasonal, festive, influencer-led, region-specific, or trend-based. Traditional production methods may not always be practical for such collections because quantities are smaller and design changes are frequent. Digital printing for limited edition textiles gives brands the flexibility to launch unique designs without committing to very large production volumes. This makes it easier to test ideas, create urgency, and respond to changing customer preferences. Small Runs Can Create Bigger Brand Value Limited edition collections often work because they feel special. Customers may respond better when a design is available only for a short time or in limited quantity. This approach can help brands build stronger engagement and reduce dependence on mass production. Digital textile printing supports this model because it allows smaller runs with high design variety. Brands can create capsule collections, festive prints, designer collaborations, custom drops, and exclusive fabric ranges with more control over production quantity. Faster Design Testing Reduces Risk Every new design carries risk. A print may look strong in concept but may not perform well in the market. With digital printing, brands can test limited quantities before committing to larger production. If a design performs well, it can be repeated. If it does not, the brand avoids large unsold inventory. This is especially useful for fashion labels, home textile brands, online sellers, and boutique businesses that need to stay fresh without overproducing. Customization Makes Collections More Attractive Limited edition textiles can become more powerful when combined with customization. Brands can create personalized prints, regional designs, special themes, or exclusive patterns for specific customer groups. Digital printing makes such customization easier because the artwork can be changed digitally without long setup processes. This helps brands create more meaningful product stories and stronger customer connection. Quality Still Defines the Collection A limited edition collection may be small in quantity, but it still needs high-quality production. Print sharpness, color consistency, fabric feel, finishing, and durability all affect how customers experience the product. Brands should work with production partners who understand both creativity and technical execution. The success of a limited edition textile collection depends on how well the design idea is converted into finished fabric. Conclusion Digital printing for limited edition textiles helps brands create exclusive collections, test new ideas, reduce inventory risk, and build stronger customer engagement. It gives textile brands the freedom to launch more creative products without being restricted by large production commitments. True Colors can support such collections by offering more than production capacity. Its ecosystem of digital printing machines, fabrics, Inkia by True Colors inks, True Colors Sublimation Paper, and technical expertise can help brands convert creative concepts into production-ready textile outputs. For limited edition collections, where every design needs to feel intentional and well-executed, True Colors brings the balance of flexibility, quality understanding, and production support that modern textile brands need.
Color Management in Textile Printing: From Design Screen to Final Fabric
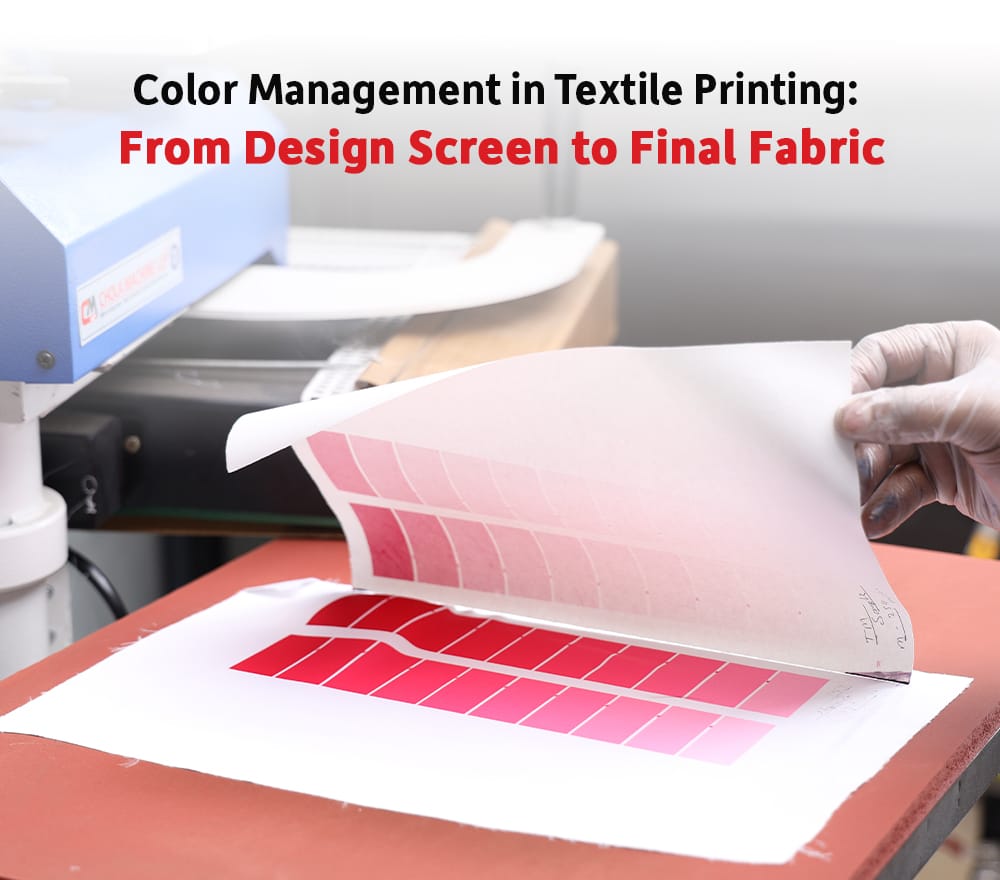
Color Changes Across the Printing Journey In textile printing, a design begins on a screen but ends on fabric. Between these two stages, many factors influence how the final color appears. Color management in textile printing helps reduce the gap between digital artwork and printed fabric. Without proper color control, manufacturers may face shade variation, repeated sampling, customer dissatisfaction, and production delays. This is why color management should be treated as an important part of the digital textile printing workflow. Screen Color Is Not Final Fabric Color Designers often approve artwork on monitors, but screen color is created through light while fabric color is created through ink, material absorption, printing process, and finishing. This means the same design can appear different on screen, paper, and fabric. Manufacturers should educate customers and internal teams about this difference. The goal of color management is not to make every screen look exactly like fabric, but to create a controlled and repeatable process that reduces unexpected variation. Fabric Type Influences Color Output Different fabrics produce different color results. Polyester, cotton, viscose, silk, blends, and other materials absorb or receive ink differently. The same print file can look brighter on one fabric and softer on another. Fabric construction, surface texture, moisture, pre-treatment, and finishing also influence final color. This is why color matching should always be tested on the actual production fabric, not only on a sample base that looks similar. Ink, Machine and Profile Must Work Together Color management depends on the relationship between ink, machine settings, RIP software, profiles, fabric, and production conditions. If one element changes, the color result may change. Manufacturers should maintain controlled settings for approved jobs and avoid unnecessary changes during repeat production. A stable workflow helps improve repeatability, especially for export orders, brand approvals, and bulk production. Sampling Helps Prevent Bulk Production Issues Sampling is an important part of color management. Before bulk production, manufacturers should print samples, review color output, check fabric behavior, and confirm customer approval. Once the sample is approved, the same settings and material combinations should be followed during production. This helps reduce shade variation and improves confidence between the printer and customer. Conclusion Color management in textile printing helps manufacturers control the journey from design screen to final fabric. It reduces shade variation, improves repeatability, and supports more reliable customer approvals. True Colors’ integrated model is especially useful for color-sensitive production because it connects multiple factors that affect final output. Machines, Inkia by True Colors inks, True Colors Sublimation Paper, fabrics, and technical support all influence color consistency in different ways. For manufacturers who struggle with repeated shade corrections, True Colors can help bring more structure to the printing process by supporting the complete production chain rather than focusing on one isolated component.